If you’ve ever worked in manufacturing, pharmaceuticals, food and beverage processing, or any industry that relies on large-scale water use, you’ve probably heard the term “water recovery rate” thrown around when talking about reverse osmosis (RO) systems. As an industrial RO system supplier, I get asked this question almost every day: “What’s the typical recovery rate for your systems?” The answer isn’t a one-size-fits-all number, and it’s not just a random statistic we pull out of a catalog. It’s a metric that balances process needs, system design, water quality, and long-term operational costs—all things we spend hundreds of hours refining when we build a system for a client. Let me break this down so you understand exactly what recovery rate means, what factors shape it, and what to expect when you’re evaluating industrial RO solutions. Industrial RO System
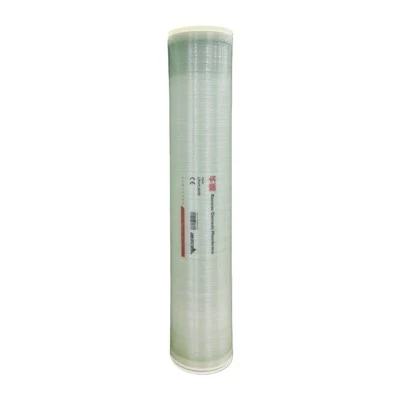
First, let’s define what water recovery rate actually is. In simple terms, it’s the percentage of feed water (the raw water you’re treating) that gets converted into usable product water, versus the percentage that becomes concentrate (often called brine or reject water, which is flushed away). For example, a 75% recovery rate means 75 gallons of feed water becomes 75 gallons of purified product, and 25 gallons is flushed as concentrate. That’s a huge difference from, say, a residential RO system, which usually has a recovery rate of just 10-15%—industrial systems are built for volume, so efficiency is non-negotiable. Why does recovery rate matter? Lower recovery means you’re wasting more raw water, paying higher water and wastewater disposal costs, and potentially increasing the environmental footprint of your operations. Higher recovery means you’re getting more out of every drop, but there’s a point where pushing recovery too hard causes problems—fouling, membrane damage, and inconsistent product water quality. That’s where our expertise as suppliers comes in: we design systems to hit the sweet spot for each client, not just the highest number possible.
Now, what’s the average recovery rate for industrial RO systems? Most standard industrial RO systems fall somewhere between 50% and 85% recovery. But that’s a broad range, and it rarely hits that 85% mark unless the feed water is exceptionally clean and the system is designed for it. Let’s contextualize that: if your feed water is municipal water with low hardness, low total dissolved solids (TDS), and minimal particulate matter, you can aim for the higher end of that range. But if your feed water is brackish groundwater (common in many industrial zones) or has higher levels of contaminants like silica, iron, or sulfate, your recovery rate will be lower, often 50-65%. Seawater RO, which is used for desalination, has even lower recovery—usually 35-50%, because seawater has extremely high TDS, and pushing recovery higher would create too much osmotic pressure that can damage membranes.
It’s important to note that 85% recovery is not a magic number, and we never quote that to a client without first auditing their feed water. Last year, we worked with a food and beverage plant that wanted to increase their recovery rate from 60% to 80% to cut their water costs. When we ran a feed water analysis, we found their source water had moderate hardness and elevated levels of organic compounds from upstream agricultural runoff. If we’d tried to push recovery to 80%, we would have seen severe fouling within 6 months—membrane pores clogging with organic matter, pressure drops spiking, and product water purity dropping below their required standards. Instead, we adjusted the design: added a better pre-treatment step (a multimedia filter with activated carbon to capture organics), optimized the membrane array to reduce concentration polarization, and set the recovery rate to 70%. The plant saved 22% on their water costs, far more than the 10% they would have saved at 80% once you factored in membrane replacement and downtime from fouling. That’s the balance we strike every time: it’s not just about raw recovery, but about long-term reliability and cost.
So what factors determine an industrial RO system’s recovery rate? Let’s go through the key ones, because this is where most clients go wrong when evaluating systems.
First, feed water quality is the biggest variable. TDS is the primary driver here. The osmotic pressure of feed water is proportional to its TDS: higher TDS means more pressure is required to push water through the membrane, which means the concentrate side gets more concentrated faster as you increase recovery. For example, a municipal water source might have a TDS of 500 ppm; its osmotic pressure is roughly 7 psi, so we can safely run recovery up to 75% before the concentrate TDS gets high enough to cause osmotic pressure issues. Brackish groundwater might have a TDS of 1,500 ppm, osmotic pressure around 22 psi, so maximum safe recovery is around 65%. Seawater has a TDS of 35,000 ppm, osmotic pressure around 500 psi, so recovery tops out at 45%—any higher, and you’d need a high-pressure pump that would outweigh the savings from reduced water use. Other contaminants matter too: silica, for example, can precipitate when concentrate is concentrated to 150-200 ppm, so if your feed water has 20 ppm silica, you can only get 7.5x concentration, which translates to a 87% recovery if silica is the limiting factor—but if you don’t have anti-scalants or filtration to prevent silica scaling, you’d never hit that. Iron, manganese, and biofouling agents will also cap recovery, because they clog membranes long before osmotic pressure becomes an issue.
Next, pre-treatment design. Pre-treatment is the unsung hero of industrial RO recovery. You can’t run a high recovery rate if your pre-treatment isn’t removing the contaminants that cause scaling and fouling. Common pre-treatment steps include multimedia filtration to remove particulates, activated carbon to remove organics and chlorine (which is deadly to RO membranes), water softening to remove hardness that forms calcium carbonate or sulfate scales, and anti-scalant injection to prevent mineral scaling. Last quarter, we worked with a textile manufacturer that had a system with 55% recovery, and their membrane supplier told them they were lucky to get 12 months out of their membranes. We did a pre-treatment audit and found they only had a simple sediment filter, no softener, and no anti-scalant. We upgraded their pre-treatment: added a cation exchange softener, a cartridge filter with 5-micron depth, and adjusted their anti-scalant dosage. Within 3 months, they increased their recovery rate to 70%, and their membranes are now lasting 24 months on average. The $12,000 investment in pre-treatment paid for itself in 8 months from reduced membrane replacement and lower water waste.
Then, the RO membrane array design. How you arrange the membranes in the system affects recovery. Most industrial RO systems use a series of membrane housings, arranged in “stages.” A standard two-stage design (the most common for brackish water) usually runs first stage at 75% recovery, and the second stage uses the concentrate from the first stage as feed water, boosting overall recovery to 85%—but only if the concentrate from the first stage doesn’t have too much TDS. Single-stage systems, which are simpler and cheaper, usually top out at 60-65% recovery, because the concentrate is too concentrated to go through a second stage. We work with clients to choose the right array: if they have clean feed water and want maximum recovery, a two-stage or even three-stage design makes sense. If they have variable feed water or are on a tight budget, a single-stage system with optimized pre-treatment might be the better choice for long-term costs. We also consider membrane type: thin-film composite (TFC) membranes, which are standard now, can handle higher concentration than older cellulose acetate membranes, so they let us run higher recovery rates without fouling.
Operating parameters also play a role in recovery. The pressure of the feed water, the cross-flow rate (the speed of water flowing across the membrane surface, which prevents scaling), and how much concentrate you reuse (many industrial plants reuse a portion of the concentrate for non-potable uses like cleaning or irrigation) all affect recovery. For example, if a plant is using concentrate for floor washing, they don’t need to flush it all away, so their effective recovery rate goes up because they’re reusing that water.
Now, what about common misconceptions about recovery rates? I hear a lot of clients say, “I need 90% recovery to save the most money,” but that’s almost never true for industrial systems. Let’s do a quick cost comparison: suppose a plant uses 1 million gallons of feed water a month, at $2 per 1,000 gallons. At 50% recovery, they use 1 million gallons, get 500,000 gallons of product, and pay $2,000 for water. At 75% recovery, they use 666,000 gallons, get 500,000 gallons, and pay $1,332 for water—saving $668 a month. At 85% recovery, they use 588,000 gallons, get 500,000 gallons, and pay $1,176, saving $156 more a month. But here’s the catch: the membrane replacement cost at 85% is 30% higher than at 75%, because of increased fouling and stress on the membranes. Add in downtime for cleaning every 3 months instead of every 6 months, and that $156 a month in water savings disappears, and often turns into a net loss. That’s why we always run a total cost of ownership (TCO) analysis, not just a recovery rate number, when designing a system.
Another misconception: “Higher recovery is always better for the environment.” That’s true in theory, but only if the concentrate you’re producing is safe to dispose of. If you’re pushing recovery so high that your concentrate has 10x the TDS of your feed water, you might not be able to discharge it to municipal wastewater, and you’ll have to pay for deep well injection or brine disposal, which is far more expensive and has a bigger environmental footprint than slightly lower recovery. We’ve had clients who wanted 80% recovery, but their local environmental agency only allows concentrate with a TDS of less than 5,000 ppm. Their feed water was 1,500 ppm, so the maximum safe concentration was 3.3x, which translates to 67% recovery. We worked with them to adjust their process: reused 20% of the concentrate for their boiler feed, and installed a small brine evaporation system for the remaining concentrate, so they hit their environmental goals without sacrificing too much water savings.
So, what should you look for when evaluating an industrial RO system’s recovery rate? First, ask for a feed water analysis: any reputable supplier will ask to test your raw water before quoting a recovery rate, not just pull a number from a data sheet. Second, ask for a TCO analysis, not just the upfront cost of the system: compare water costs, membrane replacement, pre-treatment maintenance, and downtime over 5 years, not just the first 12 months. Third, make sure the recovery rate is tied to your specific needs: if you’re a food and beverage plant needing ultra-pure water for bottling, your recovery rate will be lower than a manufacturing plant using RO for process water that doesn’t need to be as pure.
As an industrial RO system supplier, our goal isn’t to sell you the system with the highest recovery rate—it’s to sell you a system that works for your operations, saves you money over time, and meets your quality and environmental standards. We’ve seen too many plants cut corners on recovery to save a few dollars upfront, only to end up with fouled membranes, downtime, and higher long-term costs. That’s why we take the time to audit each client’s water source, their process needs, and their budget before designing a system that hits the right recovery rate.

If you’re evaluating an industrial RO system for your facility, and you want to understand the right recovery rate for your specific needs, or you’re ready to discuss upgrading your current system to improve efficiency, reach out to our team. We’ll walk you through the process, answer all your questions, and provide a custom design tailored to your operations.
Seawater Desalination RO System References
- "Reverse Osmosis: Design, Processes, and Applications for Engineers" by Tim S. Zhou
- Water Research Foundation. (2019). "Industrial Reverse Osmosis: Recovery Rate Optimization and Fouling Control"
- American Water Works Association. (2021). "Guidelines for Reverse Osmosis Systems for Industrial Applications"
- Membrane Technology and Research, Inc. (2020). "Thin-Film Composite Membranes: Performance and Recovery Limits for Brackish Water"
- World Health Organization. (2018). "Desalination for Industrial Use: Recovery Rate and Environmental Considerations"
Fujian Huamo Technology Co., Ltd.
Fujian Huamo Technology Co., Ltd. is one of the most professional industrial ro system manufacturers and suppliers in China, featured by quality products and good service. Please rest assured to wholesale the best industrial ro system made in China here and get price list from our factory. Contact us for custom service and OEM service.
Address: No.6 Hengtong Rd, Shanmei Village, Xiamei Town, Nanan City, Fujian Province, China
E-mail: info@huaromembrane.com
WebSite: https://www.hmromembrane.com/
