When I first started running my precision machining shop, we messed up a huge order for a medical device component all because of surface roughness. The part was supposed to have a super smooth finish—Ra 0.8 µm, if you’re in the game—and we came in at 1.2 µm. The client hit us hard, and we spent weeks troubleshooting, reworking parts, and losing sleep over it. That disaster taught me something: surface roughness isn’t just a “nice-to-have” spec. It’s non-negotiable for everything from aerospace fasteners to tiny electronic connectors, and getting it right separates the good precision machining shops from the great ones. Precision Machining
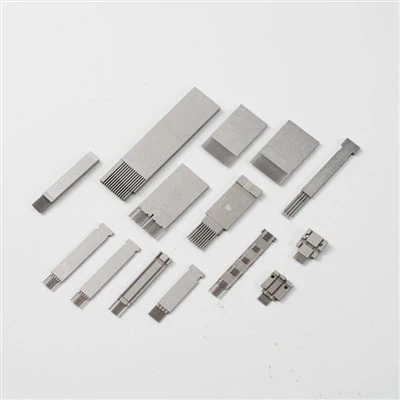
If you’re reading this, chances are you’ve dealt with that frustrating moment when a part comes off the machine looking just off—too scratched, too grainy, not smooth enough. Maybe you’ve tried cranking down the feed rate or dialing up the spindle speed, only to make things worse (trust me, I’ve been there). The truth is, improving surface roughness isn’t about random tweaks to machine settings. It’s a mix of understanding how every tiny factor plays into the finish, and making intentional, small adjustments. Over the past 10 years, we’ve refined our process so much that now we consistently hit Ra 0.4 µm without breaking a sweat, and I want to share what works for us.
First off, let’s talk about the cutting tools. This is the foundation, right? I used to grab the cheapest carbide inserts I could find, figuring “they’re all the same.” No way. The geometry of your insert—rake angle, edge radius, nose radius—does more for surface roughness than almost any other single factor. For finishing passes, we swear by positive rake angles. They reduce cutting force and friction, which means less heat built up at the cutting edge. Heat is the enemy here; it causes the tool to wear unevenly, leaving tiny notches on the part surface that show up as roughness. If you’re dealing with a hard material like titanium or Inconel, a small edge hone (or “lap”) on the insert makes a huge difference. A sharp edge might seem better, but it actually micro-chips easier in hard materials, leading to inconsistent finishes. We only use inserts with a hone size of 0.02 mm to 0.05 mm for finishing these days.
Nose radius is another big one. A larger nose radius (like 1.2 mm vs. 0.8 mm) will leave a smoother surface at the same feed rate. That’s because the contact patch between the tool and the part is wider, so the feed marks left behind are less pronounced. Wait, though—don’t crank the nose radius too high. If you’re working with a thin, flexible part, a big nose radius increases the chance of chatter, that annoying vibration that leaves wavy lines on the surface. It’s a balance, but for most precision machining jobs, a 1.0 mm or 1.2 mm nose radius is our go-to for finishing. And one rule I live by: never use a dull insert. We replace finishing inserts after just one or two parts, even if they look like they still have life. A $10 insert is nothing compared to reworking a $100 part.
Next up, machine setup and rigidity. If your machine isn’t solid, every little movement will translate to roughness. I’ve seen shops with old CNC mills that wiggle when you jog the Z-axis, and their surface finishes are terrible before they even touch the part. For precision work, we make sure our machines are calibrated quarterly—no exceptions. That means checking linear axes for backlash, spindle runout, and how well the spindle holds the tool. Even a 0.002 mm runout in the spindle will leave uneven cuts, especially on small parts. We also use shrink-fit tool holders instead of collet holders for finishing passes. Shrink fit grips the tool more evenly, reducing any wobble, which makes the cut way smoother.
Workholding is just as important. If the part isn’t clamped tightly enough, it will flex or vibrate during the cut. For tiny parts, we use soft jaws that are custom-machined to fit the exact shape of the part. A standard collet or vise jaw might have small gaps or uneven clamping pressure, which causes the part to move a tiny bit when the tool pushes into it, leaving chatter marks. For parts that are really long or thin, we use tailstocks or steady rests to support them mid-cut. Last year, we had a job for a 300 mm long aluminum rod with a 5 mm diameter, and without a steady rest, we couldn’t get below Ra 1.0 µm. Add the steady rest, and we hit Ra 0.5 µm instantly. Game changer.
Now, the settings—this is where a lot of people go wrong. I used to think “slower feed = smoother finish,” but that’s only half true. Let’s break it down. Feed rate per tooth (fz) is key here. The formula for surface roughness from feed marks alone is roughly (f²)/(8r), where f is feed per revolution and r is nose radius. So if you lower the feed, the roughness from feed marks goes down. But if you lower the feed too much, you start getting built-up edge (BUE)—that gunk that forms on the cutting edge when the material doesn’t shear cleanly. BUE leaves tiny metal chunks on the part surface, which is way worse than a few feed marks. For most finishing passes, we run feed rates between 0.1 mm/rev and 0.2 mm/rev. For harder materials, we bump it up a touch to reduce BUE.
Spindle speed is another setting to get right. Too slow, and you get more heat and BUE. Too fast, and you get vibration from high cutting speed, especially in materials that are prone to chatter. We use a simple rule: calculate the speed based on the material and tool, then test 10% higher and 10% lower to find the sweet spot. For aluminum with a carbide insert, that’s usually around 3,000–5,000 RPM. For stainless steel, it’s more like 1,500–2,500 RPM. Don’t be afraid to tweak this—small changes here make big differences.
Coolant and cutting fluids are something many shops overlook, but they’re huge. When you’re cutting at high speeds, the tool and part get hot. Coolant flushes away the chips, lubricates the cutting edge, and reduces heat. We use synthetic coolant mixed at 10% concentration (higher than the 5% people usually use) for finishing. The higher concentration gives better lubricity, which reduces friction and BUE. We also direct the coolant right at the cutting zone, not just spraying the general area. A quick tip: if you’re getting shiny spots on the part, that’s usually from insufficient lubrication—crank up the coolant concentration.
Chip evacuation is tied to coolant too. If chips get stuck between the tool and the part, they’ll scratch the surface like a file. We make sure our coolant pressure is high enough—around 100 PSI for aluminum, a bit lower for softer materials—to blow chips away. For deep holes or internal cuts, we use through-tool coolant, which pushes chips out from inside the tool, so they don’t get left behind in the hole. I can’t tell you how many scratched parts we used to get before we added through-tool coolant—fixed that problem overnight.
One trick that’s saved us so many times: taking a light semi-finish pass before the final finish pass. Most people just do one finishing pass, but a semi-finish pass removes the rough layer from the roughing cut, leaving a more uniform surface for the finish pass. We set the semi-finish depth of cut to 0.2 mm, then the finish pass to 0.05 mm. That small finish cut takes off just the uneven top layer, so the final surface is way smoother. It might add a minute or two to the cycle time, but it eliminates so many rework jobs.
Also, think about the material itself. Some materials are way harder to finish than others. Pure aluminum is a dream—super smooth, low friction. Titanium? That’s a nightmare. It’s abrasive, generates a lot of heat, and sticks to tools. If you’re working with exotic materials like Inconel or Hastelloy, you need to adjust every single thing: tool grade (we use coated carbide with high thermal resistance), spindle speed (lower than for aluminum), coolant (even higher concentration, sometimes with extreme pressure additives), and even the order of cuts. We recently finished a batch of titanium aerospace parts with Ra 0.6 µm, and the key was taking very light finish passes and replacing inserts mid-job instead of waiting for them to dull.
Wait, let’s talk about common mistakes we still make sometimes, just to be real. Last month, we tried using a cheaper collet holder for a small batch of electronic connectors, and we ended up with 20% of the parts failing roughness specs. Turned out the collet had a tiny bend, so the tool was wobbling. We switched back to shrink fit, and all the parts passed first time. Another mistake: rushing the setup. If we’re in a hurry to get a job done, we skip calibrating the machine or don’t check the tool runout, and we pay for it in rework. Taking an extra 10 minutes to set up properly saves hours later.
And here’s something you might not have thought about: the direction of the cut. For parts that will be under stress, we cut along the grain direction of the material, not against it. Cutting against the grain causes more friction and leaves a rougher surface. We also use climb milling vs. conventional milling for finishing. Climb milling means the tool cuts in the same direction as the spindle is turning, which reduces vibration and leaves a smoother finish. Conventional milling tends to push the tool into the part, causing chatter. Again, small change, big difference.
At the end of the day, improving surface roughness isn’t about fancy tech or expensive tools (though good tools help). It’s about paying attention to every tiny variable, testing small changes, and not being afraid to adjust when something isn’t working. We’ve turned that 2013 disaster into our biggest strength—now clients reach out to us specifically because we deliver consistent, smooth surfaces, no matter the material or part size.
If you’re tired of reworking parts, dealing with failed inspections, or just want to get that smooth finish you need for your application, we can help. Our precision machining team has worked with everything from medical components to aerospace parts, and we know exactly how to dial in surface roughness specs to hit your requirements on the first try. Drop a message, let us know what parts you’re working on, and we’ll send over a free quote or troubleshoot any roughness issues you’re facing. We’re here to make your jobs run smoothly, literally.
Plastic Mold References
- Astakhov, V. P. (2006). Metal Cutting Theory and Practice. CRC Press.
- DeGarmo, E. P., Black, J. T., & Kohser, R. A. (2020). Materials and Processes in Manufacturing (13th ed.). Wiley.
- Shaw, M. C. (2010). Metal Cutting Principles (2nd ed.). Oxford University Press.
- Kalpakjian, S., & Schmid, S. R. (2021). Manufacturing Processes for Engineering Materials (8th ed.). Pearson.
Dongguan Hezong Precision Technology Co., Ltd.
With abundant experience, we are one of the most professional precision machining manufacturers and suppliers in China. Please feel free to buy durable precision machining made in China here from our factory. All customized products are with high quality and competitive price.
Address: No.973, Dalang Section of Wozhang Road, Dalang Town, Dongguan City, Guangdong Province
E-mail: postmaster@hezongjingmi.com
WebSite: https://www.hzpre.com/
