Introduction to Nanofiltration Membrane
Nanofiltration (NF) membrane is a type of pressure – driven membrane filtration technology that lies between ultrafiltration and reverse osmosis. Nanofiltration membranes have pore sizes typically in the range of 1 – 10 nanometers. They are capable of selectively rejecting certain solutes based on their size, charge, and chemical properties. Nanofiltration Membrane
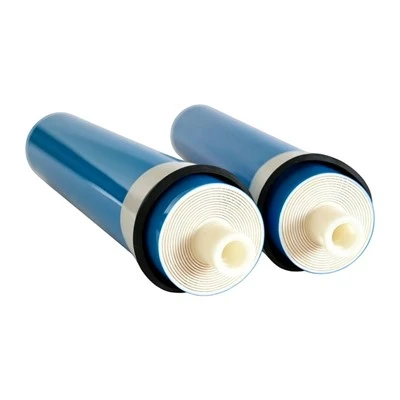
These membranes are commonly used in various applications such as water treatment, including the removal of hardness, bacteria, viruses, and some organic compounds from water. In the food and beverage industry, they are used for concentration, purification, and separation processes. Additionally, in the pharmaceutical and chemical industries, nanofiltration membranes play a crucial role in the purification and recovery of valuable products.
10 Leading Nanofiltration Membrane Manufacturers
1. Fujian Huamo Technology Co., Ltd.
Fujian Huamo Technology Co., Ltd. is a prominent player in the field of membrane technology. It has been committed to the research, development, production, and sales of high – quality membrane products. The company boasts a team of expert researchers and advanced production facilities, enabling it to continuously innovate and offer competitive membrane solutions.
Features in Nanofiltration Membrane:
- High Selectivity: Their nanofiltration membranes can precisely separate different solutes, effectively retaining substances like divalent ions while allowing monovalent ions to pass through to a certain extent.
- Good Chemical Resistance: The membranes can withstand contact with a variety of chemical substances, ensuring stability in complex industrial environments.
- Excellent Filtration Efficiency: With a uniform pore size distribution, they can achieve high – flux filtration, increasing the productivity of water treatment and separation processes.
Advantages:
- In – house R & D: The company invests heavily in research and development, which allows it to quickly adapt to market demands and develop new membrane products with improved performance.
- Quality Assurance: Strict quality control systems are in place throughout the production process, ensuring that each membrane product meets high – quality standards.
- Customer – oriented Service: Huamo Technology provides comprehensive technical support and after – sales service, helping customers solve problems in time.
Website: https://www.hmromembrane.com/
2. Dow Chemical Company
Dow is a global chemical giant with a long – standing history and rich technical expertise. It has a significant presence in the membrane technology market. The company’s broad product portfolio and strong R & D capabilities enable it to offer high – performance nanofiltration membranes.
Features in Nanofiltration Membrane:
- Advanced Material Science: Dow uses proprietary materials in its nanofiltration membranes, which provide excellent mechanical strength and durability.
- Customization: They can customize membranes according to different industrial needs, such as specific filtration requirements for different types of wastewater.
- Energy – efficient Design: The membranes are designed to operate at relatively low pressures, reducing energy consumption during the filtration process.
Advantages:
- Global Reach: Dow has a vast global distribution network, ensuring that its products can be quickly delivered to customers around the world.
- Research Collaboration: The company collaborates with leading research institutions, which helps it stay at the forefront of membrane technology development.
- Brand Reputation: Dow’s long – established brand is associated with high – quality and reliable products, giving customers confidence in their purchases.
3. Toray Industries, Inc.
Toray is a well – known Japanese company with a focus on advanced materials. In the field of nanofiltration membranes, it has made significant contributions through continuous innovation and high – quality production.
Features in Nanofiltration Membrane:
- High – performance Separation: Toray’s nanofiltration membranes can achieve high – precision separation of various substances, especially in the field of water purification for sensitive applications.
- Antifouling Properties: The membranes are engineered to resist fouling, which extends their service life and reduces the frequency of cleaning and maintenance.
- Thermal Stability: They can operate stably under a certain range of temperatures, which is beneficial for industrial processes that require thermal treatment.
Advantages:
- Integrated Production System: Toray has an integrated production system, from raw material production to final membrane manufacturing, which allows for better quality control and cost – effectiveness.
- Environmental Awareness: The company is committed to developing environmentally friendly membrane products, meeting the growing demand for sustainable solutions.
- Strong Technical Support: Toray provides in – depth technical support to help customers optimize the use of their membranes.
4. Koch Membrane Systems
Koch Membrane Systems is a leading provider of membrane filtration products and solutions. It has a wide range of applications in industries such as food and beverage, pharmaceuticals, and water treatment.
Features in Nanofiltration Membrane:
- Wide Range of Configurations: They offer different membrane configurations such as spiral – wound and tubular, which can be selected according to specific process requirements.
- High Precision Filtration: Koch’s nanofiltration membranes can achieve precise separation of molecules with different molecular weights, which is crucial for the purification of high – value products.
- Scalability: The products can be easily scaled up from laboratory – scale to industrial – scale production, meeting the needs of different – sized enterprises.
Advantages:
- Industry – specific Solutions: Koch has in – depth understanding of different industries and can provide tailored membrane solutions for specific industry challenges.
- Long – term Experience: With decades of experience in the membrane industry, Koch has a proven track record of providing reliable products.
- Service Network: A comprehensive service network ensures quick response to customer problems and on – site support.
5. GE Water & Process Technologies (now SUEZ)
GE, and later acquired by SUEZ, has a long – standing history in water treatment technology. Their nanofiltration membrane products are widely used in large – scale water treatment projects.
Features in Nanofiltration Membrane:
- Robust Design: The membranes are designed to be durable and resistant to physical and chemical stresses, suitable for harsh operating conditions.
- High – capacity Filtration: They can handle large volumes of water or fluid with high – throughput filtration, which is ideal for municipal and industrial water treatment applications.
- Smart Monitoring Technology: Some of their products are equipped with smart monitoring capabilities, allowing real – time monitoring of membrane performance and early detection of potential problems.
Advantages:
- System Integration: GE/SUEZ can provide complete water treatment systems, integrating nanofiltration membranes with other treatment processes for more efficient operations.
- Large – scale Project Experience: The company has extensive experience in implementing large – scale water treatment projects around the world, which gives it an edge in handling complex projects.
- Research and Development Resources: It has significant R & D resources dedicated to continuously improving membrane performance and developing new applications.
6. Alfa Laval
Alfa Laval is a global leader in heat transfer, separation, and fluid handling technologies. In the field of nanofiltration membranes, it combines its expertise in fluid dynamics and separation to offer innovative solutions.
Features in Nanofiltration Membrane:
- Efficient Fluid Handling: The membranes are designed to optimize fluid flow, reducing pressure drop and improving overall filtration efficiency.
- Hygienic Design: Ideal for applications in the food, beverage, and pharmaceutical industries, the membranes are designed to meet strict hygiene standards.
- Modular Design: Alfa Laval’s membrane systems feature a modular design, which allows for easy installation, expansion, and maintenance.
Advantages:
- Multidisciplinary Expertise: The company’s knowledge in multiple fields such as heat transfer and fluid handling enables it to develop more comprehensive membrane solutions.
- Global Customer Base: With a large global customer base, Alfa Laval has a deep understanding of different customer needs and can provide customized solutions.
- Sustainable Solutions: The company is committed to developing sustainable membrane technologies that reduce energy consumption and waste generation.
7. Hydranautics (a Nitto Group Company)
Hydranautics has a strong reputation for manufacturing high – quality membrane products. It focuses on providing reliable nanofiltration solutions for various industries.
Features in Nanofiltration Membrane:
- Low – pressure Operation: Their membranes can operate at relatively low pressures, which reduces energy costs during the filtration process.
- High – quality Separation: They offer excellent separation performance, effectively removing contaminants and impurities from water and other fluids.
- Long Service Life: Due to the high – quality materials and manufacturing processes, the membranes have a long service life, reducing replacement costs.
Advantages:
- Research and Development Focus: Hydranautics invests a lot in R & D to continuously improve the performance of its membranes and develop new membrane materials.
- Technical Training: The company provides technical training for customers to ensure the correct use and maintenance of their membranes.
- Quality Certification: Its products are certified to meet various international quality standards, ensuring product reliability.
8. Toyobo Co., Ltd.
Toyobo is a Japanese company with a diverse range of businesses, including membrane technology. Its nanofiltration membrane products are known for their quality and performance.
Features in Nanofiltration Membrane:
- Charge – based Separation: The membranes can utilize charge – based separation mechanisms, which provide an additional dimension for precise separation of solutes.
- Flexible Design: Toyobo can design membranes with different layer structures and properties to meet the specific requirements of different applications.
- Good Chemical Compatibility: The membranes are compatible with a wide range of chemicals, which makes them suitable for various industrial processes.
Advantages:
- Material Innovation: The company is at the forefront of material innovation, constantly developing new membrane materials with improved properties.
- Quality Control: Stringent quality control measures ensure that each membrane product meets high – quality standards.
- Collaborative Development: Toyobo collaborates with customers to develop customized membrane solutions that precisely meet their needs.
9. Microdyn – Nadir GmbH
Microdyn – Nadir is a European company specializing in membrane technology. It offers a comprehensive range of membrane products, including nanofiltration membranes.
Features in Nanofiltration Membrane:
- Surface Modification Technology: The company uses surface modification technology to improve the antifouling and separation performance of its membranes.
- High – purity Filtration: Their nanofiltration membranes can achieve high – purity filtration, which is crucial for applications in the pharmaceutical and electronics industries.
- Easy Installation and Maintenance: The membrane modules are designed for easy installation and maintenance, reducing downtime for industrial processes.
Advantages:
- European Quality Standards: Microdyn – Nadir adheres to strict European quality standards, ensuring the high quality and reliability of its products.
- Specialized Technical Support: The company provides specialized technical support for different industries, helping customers solve complex filtration problems.
- Continuous Improvement: It is committed to continuous improvement of its membrane products through research and development efforts.
10. Synder Filtration
Synder Filtration is a well – known US – based company in the membrane filtration industry. It focuses on providing cost – effective and high – performance nanofiltration solutions.
Features in Nanofiltration Membrane:
- Economical Design: The membranes are designed to be cost – effective without sacrificing performance, making them suitable for small and medium – sized enterprises.
- Diverse Pore Size Options: Synder offers a variety of pore size options in its nanofiltration membranes, which can be selected according to different separation requirements.
- Good Chemical and Physical Stability: The membranes can maintain stable performance under different chemical and physical conditions.
Advantages:
- Customer – centric Approach: The company focuses on understanding customer needs and providing personalized membrane solutions.
- Prompt Delivery: Synder has an efficient production and delivery system, ensuring prompt delivery of products to customers.
- Technology Transfer: It is willing to transfer relevant membrane technologies to customers, helping them improve their own separation processes.
High Temperature EDI Module In conclusion, these 10 manufacturers are leading the way in the nanofiltration membrane industry in 2026, each with its own unique features and advantages, and they are pushing the boundaries of nanofiltration technology through innovation and continuous improvement.
